How Much Does Die Design Affect Die Cost and Life?
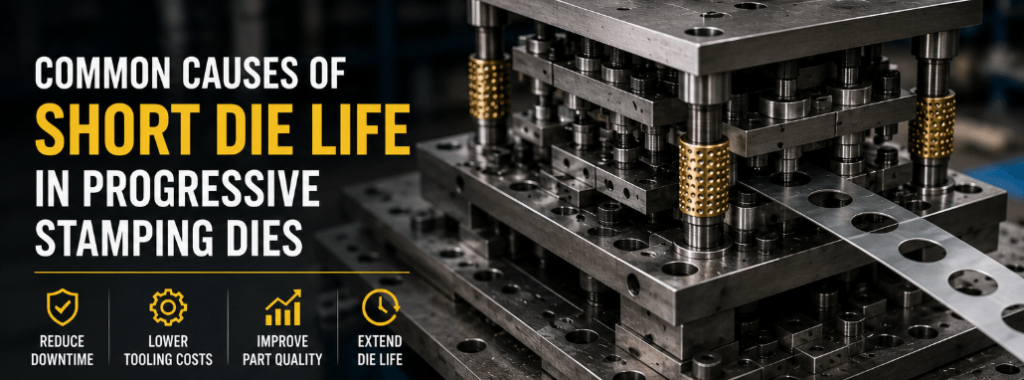
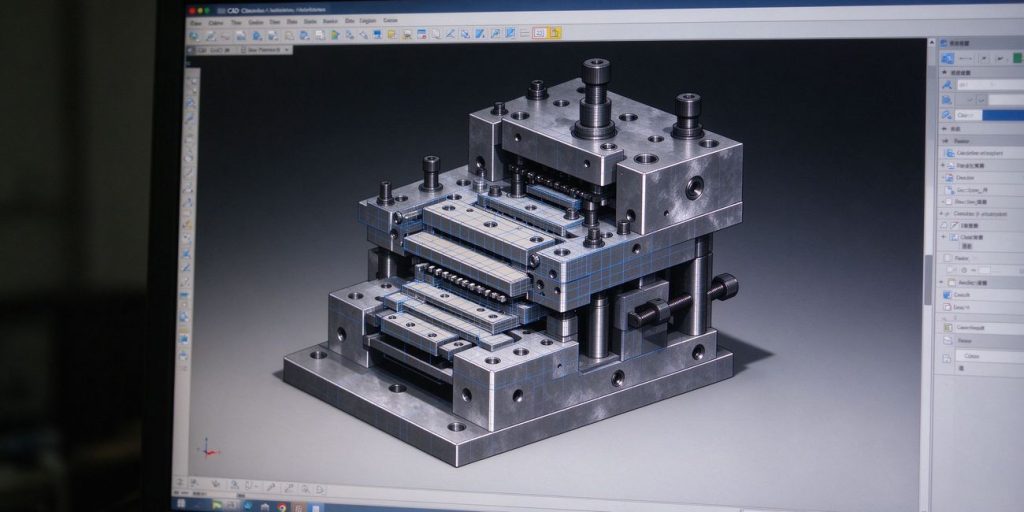
Die design is the leverage point—but not the only factor. Two suppliers can quote the same die on different design routes and end up in different cost and service-life brackets. Material, machining, and shop-floor maintenance all play their part. The design stage controls how much leverage each of those later factors gets. Die design means the layout of stations, where the material flows, the tolerances assigned to each feature, and the wear surfaces planned into the die. None of those decisions appear on the part drawing. All of them show up in the final number and in how many strokes the die survives. How Die Design Choices Translate into Cost A die’s number is mostly set before the first cut is made. The same part can run on two very different design routes. A simple single-station die, or a multi-station progressive layout, can put the number in a different bracket. Material, structure, tolerance split, and wear-surface planning each push that number in a different direction. Most buyers only see the final figure. The useful move is recognizing which design choices drive it. Those are the levers you can still adjust before tooling starts. The choices below separate two groups: the ones that really move the number, and the details that add shop-floor hours without buying anything. Which Parts of Stamping Dies Design Move Cost the Most? Stamping die design has several cost drivers, but they do not weigh equally. Roughly speaking: Design decision Impact on die design cost Impact on tool life Number of stations and strip layout High — more stations mean more machining and fitting hours Medium — more stations raise alignment demands Tolerance split across features High — tight limits push grinding and wire EDM time up Medium Wear-surface material choice Medium — better steel costs more per block High — directly sets wear rate Replaceable-insert layout Medium — slightly more detail to machine High — fast swap means longer effective life Guidance and datum scheme Medium High — good alignment slows wear on every station Cosmetic chamfers and non-functional details Low Low The first three rows pay back attention. The last row usually buys nothing. Die design for manufacturability — checking geometry against how the shop will actually grind, EDM, and fit the die — keeps the middle rows honest. Why Do Die Design Iterations Waste the Most? Die design iterations are the silent cost driver. Changing a sketch on screen costs hours. Changing a finished insert costs days, plus a new tryout round. Most expensive iterations come from the same few causes: Choosing a strip layout before the part’s critical features are locked. Not checking clearance and springback assumptions against the real material grade. Tight limits copied to every station “just to be safe.” Progressive die design makes this worse by default: one redesign ripples through every downstream station. A layout review with the machining side — how die layouts are reviewed before build — catches most of these before steel is cut. How Die Design Shapes Tool Life Cost answers the first question. Tool life answers the second — what the die looks like by its millionth stroke. A die that runs well on day one can still drift, chatter, or wear early. That happens when the layout did not plan for wear from the start. The same design choices that set the budget also decide where wear concentrates. They set how fast the edge rolls over, and how easy the die is to repair between runs. Wear is never fully avoidable. The question is where the die wears, and whether fixing it takes a ten-minute insert swap or a week on the bench. The next subsections map the common wear points to the design choices behind them. Where Does Die Wear Start, and Can Design Redirect It? Most die wear concentrates in three places, and each has a design answer: Cutting edges — punch and die clearance, edge geometry, and material-flow angle determine how quickly the edge rolls over. Material-flow surfaces — where strip drags hardest. Radius choice, surface finish, and edge breaks keep the flow smooth. Guidance parts — pillars, bushings, and pilot buttons. Misalignment here accelerates wear at every station above it. Design cannot remove wear. It can shift wear to a cheap-to-repair spot —a replaceable insert beats a reground block every time. Which Choices Buy the Longest Die Life? Die life expectancy is not a single number. It depends on run volume, material abrasiveness, and how the die is maintained. Within those boundaries, a few design choices consistently pay off: Plan wear-prone stations as inserts from day one, not as an add-onafter the first failure. Material grade matched to the duty — premium steel where it works hardest, standard steel elsewhere. Clearance and geometry reviewed against the actual strip, not a textbook table. Maintenance access built in — cleaning and adjustment at the press, not on the bench. None of these doubles life on its own. Together, over a long run, they extend the die’s effective service life by a meaningful margin—typically depending on material grade and stroke count. Before tooling starts, run five checks against the layout: Are the part’s truly critical features marked, and do the strip stations land on them? Are tolerances split by function, not blanket-tight across every station? Where will wear concentrate, and are those surfaces inserts? (This ties directly into how die layouts are reviewed before build.) Has the material grade been matched to the wear surfaces, not just to price? Can maintenance reach the working surfaces without stripping the whole die? Die design doesn’t decide cost and life on its own. It decides which later factors you pay for, and which ones you fight. Get the five checks above right before steel is cut, and the cost and life numbers you compare later will mean something. Skip them, and the cheapest bid becomes the most expensive one to run.